Our Facilities & Capabilities
At ATR Seeds, everything happens under one roof, from sourcing and cleaning, through to mixing, packing and dispatch. Our purpose-built seed operation is designed for speed, flexibility and complete control.

Secure Supply Chain, Reduced Risk.
We actively help reduce your exposure to stock risk and supply uncertainty.
Large on-site stockholding for immediate availability
Ability to store seed (mixed or unmixed) on your behalf
Flexible ordering, buy what you need, when you need it
Direct-to-customer (own-bag) fulfilment available
This allows you to operate leaner, without tying up capital in stock.
Built for Speed.
Designed for Flexibility.
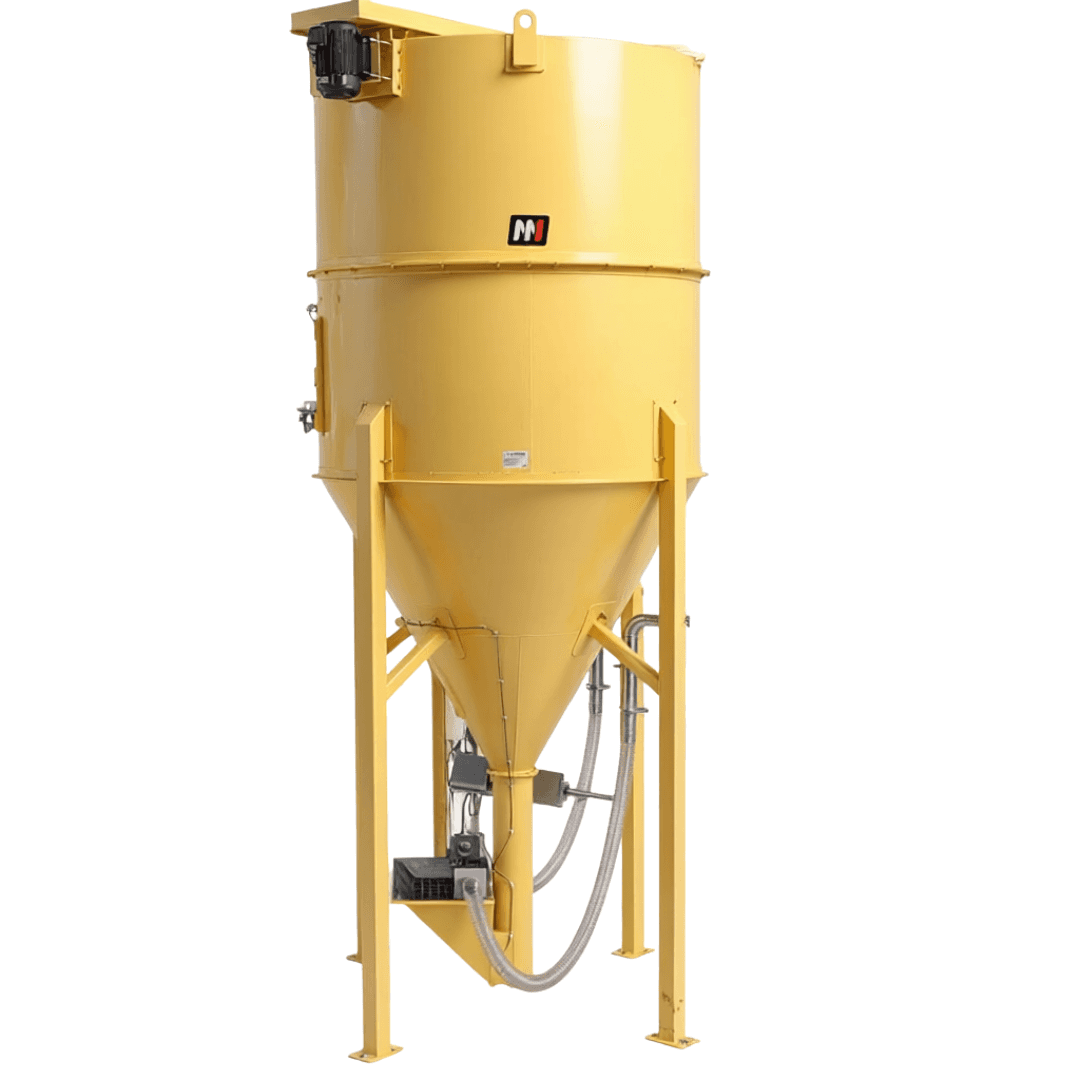
Our facility is built to respond quickly to customer demand with traceability and quality assured. We have 12 dedicated mixing lines and capacity to mix 120+ tonnes per day.
We have the UK’s largest seed mixer (12-tonne capacity)
We have full flexibility to offer quick one-off samples to full-scale production runs, with turn around same-day or next-day.
From Intake to Dispatch, Seamlessly Managed
Our integrated system tracks every stage:
Seed intake and quality control
Cleaning and preparation
Mixing and batch allocation
Packing and labelling
Storage or immediate dispatch
With everything managed on-site, we eliminate delays, reduce handling risk, and maintain full accountability throughout.

A Partner Built
Around Your Business
ATR Seeds is designed to support your operation, not complicate it.
With large-scale capability, flexible fulfilment, and a non-competing model, we give you the tools to grow your offering without increasing your risk.
ATR Seeds does not sell direct to end users, giving you complete confidence that your customers remain yours. Our role is to support your business with reliable product, flexible supply, and consistent quality.
A Simple Promice
Quality. Service. Speed.
Everything we do is built around delivering these three things, consistently, reliably, and at scale.